How are disposable vapes manufactured? The answer involves more than fitting a battery into a colored shell. Production usually combines component sourcing, electronic assembly, liquid filling, device sealing, and quality checks. Exact processes vary by manufacturer and product design, so no single factory workflow represents the entire industry.
A typical device contains a battery, control circuitry, a heating element, a wick, and a mouthpiece. These parts are assembled with attention to fit and consistency. Workers or automated systems may inspect solder joints, check airflow, and verify that the casing is properly sealed. Filling and packaging are controlled steps, too. A small leak or loose connection can affect performance. Small details matter.
The phrase how are disposable vapes manufactured also raises questions about traceability and quality assurance. Responsible explanations should distinguish documented practices from marketing claims. They should not imply that every product receives identical testing or that manufacturing alone proves a device is safe. That distinction is easy to miss.
A named expert quotation should be verified against a reliable interview or publication. No source for such a statement was provided, so attributing a quote here would risk inventing evidence. This article can instead examine the production stages, common inspection points, and the limits of what public information can confirm. Some factory details remain undisclosed. That deserves scrutiny, not guesswork.
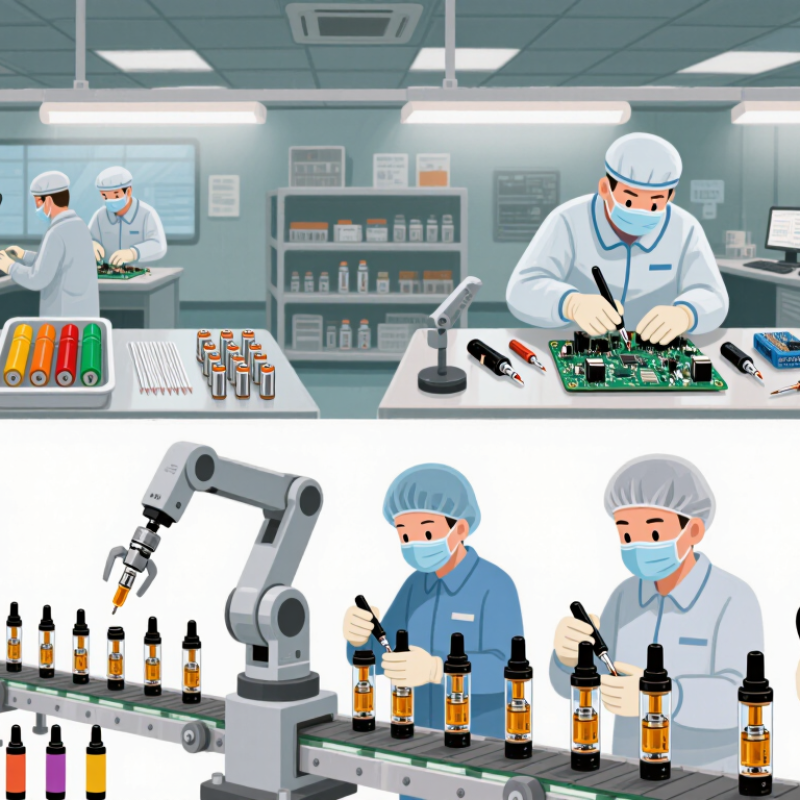
Disposable vape design starts with the user’s hand, not just a drawing. Engineers check the mouthpiece shape, airflow path, device weight, and visible liquid level. A small prototype can reveal problems early. For example, a tight air channel may make each draw feel inconsistent, while a loose seal can cause leakage. Teams should test fit, durability, and performance across repeated samples, not rely on one polished unit.
Compliance needs to shape the design from the beginning. Requirements differ by destination market and may cover product registration, permitted ingredients, emissions, warning labels, and battery safety. Manufacturers should keep traceable records for materials, suppliers, test results, and production changes. Independent laboratory testing can help verify that a finished device matches its documentation. A tiny gap matters. Even a clear label can become unreadable when printed on a curved, glossy surface.
Battery protection, reliable seals, and controlled assembly deserve careful checks on the production line. Inspectors can examine solder joints, airflow, and leakage, then record defects by batch. Packaging should carry accurate information and avoid unsupported performance claims. A design can look refined yet still be difficult to recycle; that trade-off is easy to overlook. Teams should review it openly, alongside safety and market-specific compliance, before approving production.
Sourcing disposable-vape components starts with a compact bill of materials: a battery cell, metal contacts, a heating element, a wick, a liquid reservoir, seals, and a polymer casing. Suppliers need to document material specifications and batch traceability, not just unit prices. Small parts matter. Variations in seals or reservoir plastics can affect leakage and product consistency, so incoming checks should match written specifications.
Battery sourcing connects the product to wider mineral supply chains. The International Energy Agency’s Global Critical Minerals Outlook 2024 reports that lithium demand rose by 30% in 2023. That figure does not describe vape batteries alone, but it shows why suppliers should ask for clear material and safety documentation. For casings and reservoirs, polymer choice also deserves scrutiny. The OECD’s Global Plastics Outlook reports that global plastics production reached 460 million tonnes in 2019, while only 9% of plastic waste was ultimately recycled.
Certificates help, but they do not prove every upstream claim. A tidy spreadsheet can still miss a subcontractor. Manufacturers should check supplier records, component consistency, and packaging claims, then keep evidence linked to each production batch. It is unglamorous work. It is also easy to overlook.
This illustrative map shows how often each material family appears across seven typical component groups: enclosure, liquid reservoir, seals, heating assembly, battery, circuit board, and wick. Groups may contain more than one material family. Counts are not market shares or a universal bill of materials; designs vary.
A disposable vape’s battery, control circuit, and heating system are assembled as one compact unit. The battery is positioned inside an insulated compartment, with its contacts connected to the circuit board. Workers or automated stations check polarity and connection strength. The circuit regulates power and may include safeguards against short circuits or excessive current. Small parts leave little room for mistakes.
The heating element is aligned with an absorbent wick and the airflow path. When activated, the circuit sends power to the element, which warms the liquid held in the wick. Production checks can measure electrical resistance, inspect solder joints, and confirm consistent airflow. A misaligned wick can heat unevenly. That can affect performance, even when the outer casing looks perfect. No assembly line is flawless, so traceable checks matter.
Tips: Look for clear quality-control steps, not just a fast production claim. Battery insulation, stable electrical connections, and consistent heating are practical points to verify. Sample testing helps catch faults, but it cannot guarantee every unit is identical. Manufacturers should review failed tests and improve the process. That part is often overlooked.
Filling starts only after the reservoir, wick, and contact points pass visual checks. A clean, controlled area helps limit dust and handling contamination. Calibrated equipment dispenses the specified liquid while operators watch for bubbles, uneven levels, or residue near the opening. Small differences matter. An automated reading can catch volume drift, but it cannot explain every unusual result.
After filling, the opening is closed with a fitted seal or cap, then the outer body is joined. Alignment checks help confirm that the closure sits evenly. A brief hold gives staff time to look for seepage around seams and air inlets. It is not glamorous work. Yet a rushed seal can turn a sound component into a leaky device.
Testing follows in batches, with individual units sampled for closer inspection. Workers may check electrical continuity, activation response, airflow, and visible leakage using controlled procedures. Results are recorded by production lot, helping teams trace recurring faults to a component or station. Failed devices are separated from the line. Even careful checks have limits; handling after testing can reveal weaknesses, so teams should also question whether their inspection methods are catching the right problems.
| Manufacturing Stage | Typical Operation | Quality Checks and Records | Why It Matters |
|---|---|---|---|
| Component receiving | Incoming parts may include the housing, battery, heating element, wick, mouthpiece, seals, and electronic components. Materials are checked against the product specification before assembly. | Visual inspection, part identification, dimensional checks where specified, and supplier-lot traceability. | Defective or mismatched parts can affect fit, electrical function, leakage control, and product consistency. |
| Battery and circuit assembly | The battery and control components are fitted into the device assembly. Electrical connections are made according to the design, with insulation and spacing maintained as specified. | Checks can include polarity, connection quality, short-circuit screening, and verification that the relevant battery safety requirements are met. | Helps reduce risks associated with poor connections, unintended activation, or battery failure. |
| Heating element and wick installation | The heating element and liquid-delivery material are positioned and connected to the airflow and electrical design of the device. | Position, secure fit, electrical continuity, and consistency with the approved assembly specification are checked. | Correct placement supports reliable liquid delivery and consistent device operation. |
| E-liquid filling | Where the product is designed to be filled on the production line, a metered filling system dispenses the specified liquid quantity into the reservoir or absorbent material. | Fill quantity is checked using the production control method; operators also inspect for spills, contamination, and incorrect material identification. | Controlled filling helps maintain consistency and limits contamination or overfilling. Formulation and permitted ingredients depend on the product and destination-market rules. |
| Sealing and closure | The reservoir, housing, mouthpiece, and other closure parts are assembled using the product’s specified joining or sealing method. | Visual inspection of seams and closures, fit checks, and leak screening using the applicable inspection procedure. | A sound closure helps prevent liquid leakage and protects internal components during handling and transport. |
| Firmware and activation checks | For devices with electronic controls, the production line verifies the configured control functions and activation behavior described in the product specification. | Functional checks may cover activation response, indicator operation where fitted, and automatic shut-off features where specified. | Confirms that electronic functions operate as intended for the particular design. |
| Airflow and output testing | Finished devices or samples are checked for airflow and basic operation using the manufacturer’s defined test method. | Test results are compared with the applicable product specification; unusual draw resistance, failure to activate, or inconsistent operation can trigger investigation. | Helps identify assembly or airflow-path problems before products are released. |
| Leak and appearance inspection | Devices are inspected after assembly for visible damage, residue, loose parts, and signs of leakage. Some production plans include a defined holding period before reinspection. | Inspection findings are recorded by lot, with nonconforming units separated for review or disposal. | Supports product integrity and helps prevent visibly damaged or leaking units from entering packing. |
| Final sampling and release | Quality staff review production and test records and perform checks on finished units according to the lot-control plan. | Records can include inspection results, test outcomes, material lots, nonconformance actions, and release authorization. | Traceable records help manufacturers investigate defects and demonstrate that defined production controls were followed. |
| Packaging and labeling | Accepted devices are packed and labeled according to the intended market and product requirements. | Checks include packaging condition, label accuracy, required warnings, and consistency between the product and its documentation. | Packaging protects the device and supports compliance with applicable destination-market requirements. |
| Note: This table describes common production and quality-control stages at a general level. Equipment, test methods, product specifications, and legal requirements vary by design and destination market; this is not a universal factory process specification. | |||
Packaging is the first practical checkpoint in a disposable vape supply chain. At a Chinese manufacturing site, finished units may be packed into individual cartons, then grouped into sealed outer cases. Labels can identify the product type, production batch, and inspection date. Clear print matters. A smudged code can slow receiving checks or make a carton harder to trace. Packaging also needs to protect devices from dust, impact, and moisture during storage and transport.
Traceability depends on records that connect each batch with its inspection and shipment details. A case code can help warehouse staff compare physical stock with digital records. Distributors can record dispatch dates, quantities, and destination warehouses. These steps support stock rotation and make discrepancies easier to investigate. In practice, records can be incomplete or labels can be damaged, so routine checks still matter. No system is flawless.
Tips: Check that carton codes are readable before dispatch. Match case counts against shipping records. Store cartons in a clean, dry area, and keep batch information accessible to receiving staff.
Mouthpiece shape, airflow, weight, and liquid visibility all matter. A narrow air channel may make draws feel uneven.
Requirements vary by market and may cover ingredients, labels, emissions, registration, and battery safety. Records should track materials, suppliers, tests, and design changes.
Inspect insulation, polarity, solder joints, and connection strength. The circuit should include suitable safeguards. Small parts leave little room for mistakes.
Check the heating element’s alignment with the wick and airflow path. Electrical resistance and airflow tests may reveal problems. A perfect-looking casing proves little.
Use calibrated equipment and a clean work area. Watch for uneven liquid levels, bubbles, and residue near the opening.
Confirm the seal sits evenly, then inspect seams and air inlets for seepage. Not glamorous work. Rushed checks can miss a weak seal.
Sample units for continuity, activation response, airflow, and visible leaks. Recording results by production lot can help trace repeated faults.
No. Samples can catch some faults, but not every unit is identical. Handling after testing may expose weaknesses, so inspection methods deserve regular review.
How are disposable vapes manufactured? The process begins with product design, where manufacturers define the device’s size, function, materials, and performance targets while checking that the design meets applicable quality and safety requirements. They then source components such as the outer casing, battery, electronic circuit, heating element, and absorbent material, along with materials selected for consistency and durability.
During assembly, the battery, circuit, and heating system are fitted into the casing and inspected for correct connections. The device is then filled with its intended liquid, sealed to reduce leakage, and tested for basic function, airflow, and assembly quality. Finally, each unit is packaged with suitable product information and identifying details. Traceability records help manufacturers track materials and production batches, while distribution procedures support orderly handling and delivery. Throughout the process, consistent inspections help ensure that devices meet defined specifications before they leave the facility.
Flow Vape